Leave Your Message
In the rapidly evolving landscape of global healthcare, Elderberry Extract (Sambucus nigra) has transcended its traditional origins to become a cornerstone of both pharmaceutical and herbal remedy sectors. As a high-value botanical intermediate, its application in viral defense and immune modulation has positioned it as a critical raw material for biotech and pharmaceutical manufacturers worldwide.
Unlike standard food-grade powders, Elderberry Extract for pharmaceutical use requires rigorous standardization of Anthocyanins and Polyphenols. Research indicates that specific flavonoids in elderberry bind to the H1N1 virion, effectively blocking viral entry into host cells. This mechanism of action is currently being explored in advanced pharmaceutical formulations to create synergistic effects with synthetic antivirals.
The global market for Elderberry Extract is witnessing a compound annual growth rate (CAGR) exceeding 7%. This surge is driven by a paradigm shift in consumer behavior—moving from reactive treatment to proactive immune maintenance. China, as a global hub for botanical extraction, has integrated advanced peptide technology with traditional herbal processing, creating a new generation of "Peptide-Herbal" hybrid supplements.
For pharmaceutical companies, the stability of the supply chain is paramount. The industry is moving toward vertically integrated models where raw material sourcing, extraction purity (HPLC verified), and GMP-compliant manufacturing are handled under one roof. Rongchuang International Co., Ltd. leverages China’s mature chemical industry chain to provide a consistent supply of these high-purity extracts, ensuring that research institutions and drug manufacturers have the reliable pillars they need for production.
While immune support is the primary driver, deeper application scenarios are emerging in Metabolic Health and Anti-Aging. The high antioxidant capacity of Elderberry Extract is being utilized to combat oxidative stress in chronic metabolic disorders. Furthermore, its inclusion in GLP-1 related support protocols is a growing trend, helping to manage systemic inflammation in patients undergoing metabolic treatments.
In the herbal remedies sector, the "50:1" or "Standardized 25% Anthocyanins" labels are no longer sufficient for professional-grade products. Modern pharmaceutical intermediates require batch-specific HPLC (High-Performance Liquid Chromatography) profiles. This level of precision ensures that the bioactive compounds are present in therapeutic dosages, allowing for predictable clinical outcomes in herbal medicine formulations.
Rongchuang International is a global supplier specializing in pharmaceutical intermediates, chemical raw materials, and high-value peptide products. Based in China and serving the world, we are committed to providing high-quality raw material solutions for pharmaceutical companies, research institutions, and biotech companies.
Since its establishment, we have always focused on the field of metabolic health, deeply investing in the four golden tracks of weight loss, anti-aging, hypoglycemic, and anti-fatigue. With a profound understanding of China's chemical industry chain and a keen insight into the international market, we have become an important part of the global GLP-1 and related peptide raw material supply chain.
Learn More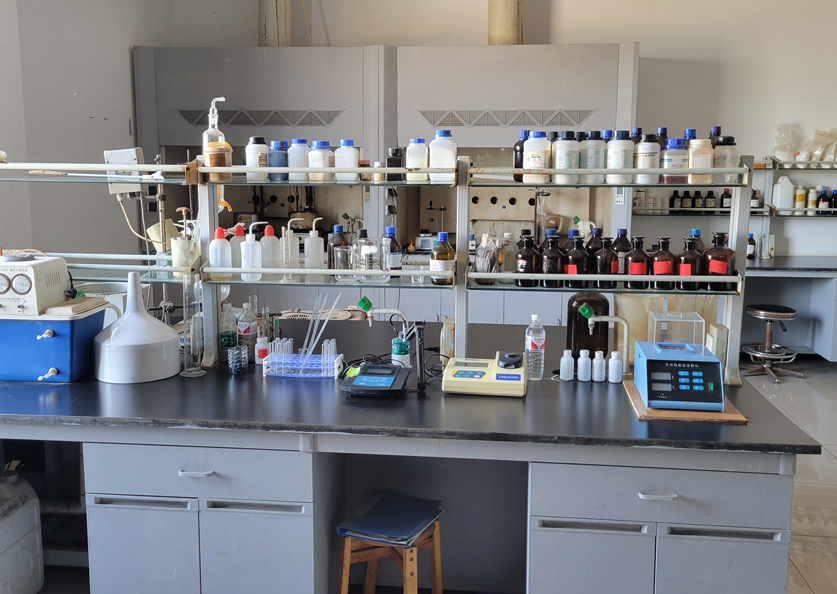
All products strictly follow quality control standards, with purity reaching ≥99%. Batch testing, providing HPLC/GC analysis certificate (COA). Produced in accordance with GMP standards.
Relying on China's mature peptide industry chain and large-scale production capacity. Strategic partnerships with high-quality manufacturing enterprises.
Familiarity with compliance requirements for export. Assistance in handling "Export Permits" and comprehensive document support for regulatory approvals.
From basic chemical raw materials to pharmaceutical intermediates. One-stop supply chain solution with pre-sale consultation and post-sale technical support.
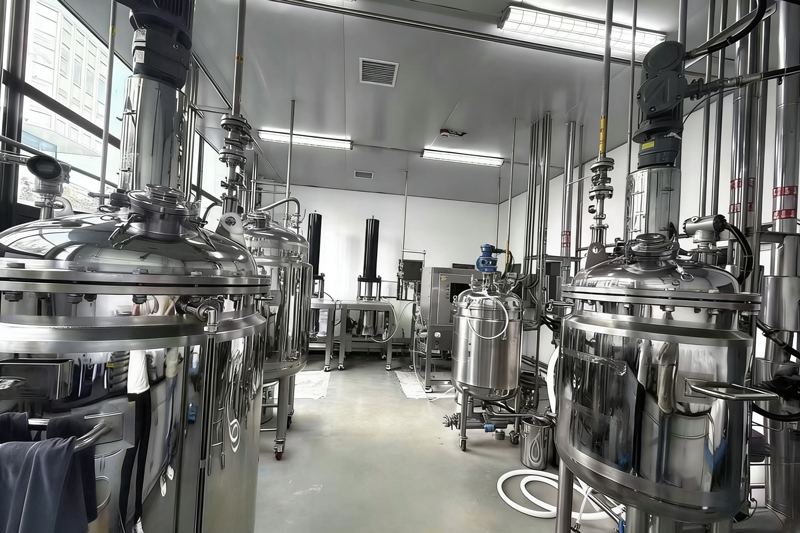
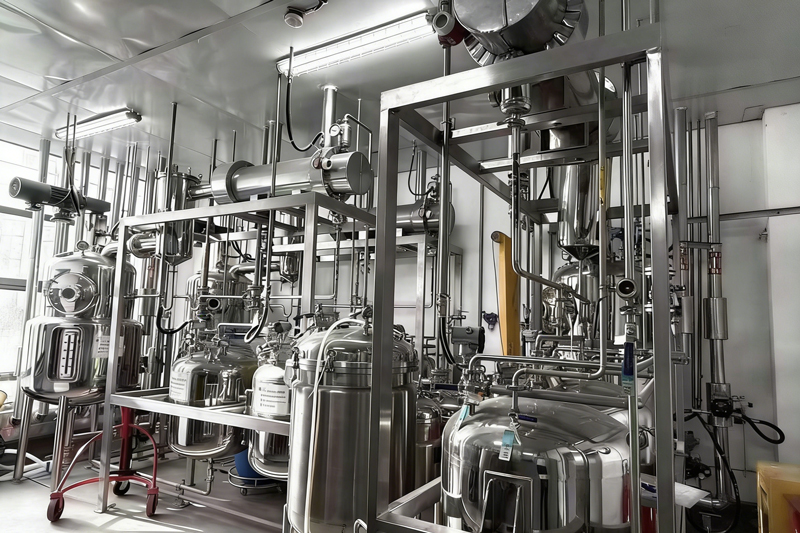
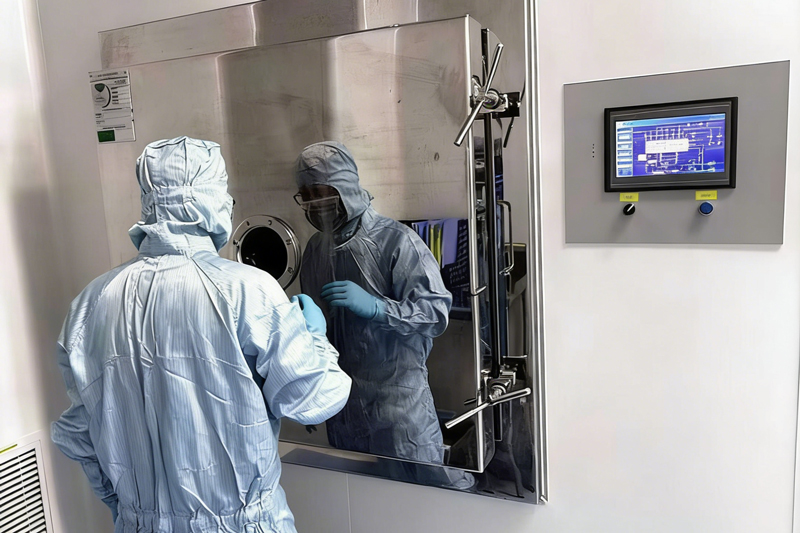
Our products have been exported to North America, Europe, Southeast Asia, Japan, and South Korea. We serve pharmaceutical enterprises, biotechnology companies, research institutions, and trade partners worldwide.
"To provide a reliable raw material support for global health endeavors." We believe that behind every life-changing drug, there is no shortage of high-quality raw materials. We are the silent pillar supporting global partners.
Contact Us Now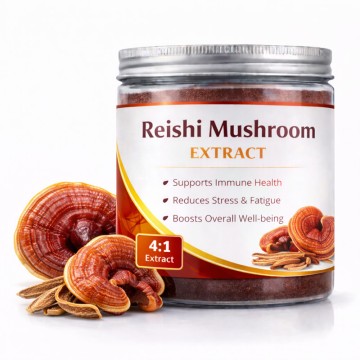 Reishi Mushroom Extract Anti-Fatigue Ingredient
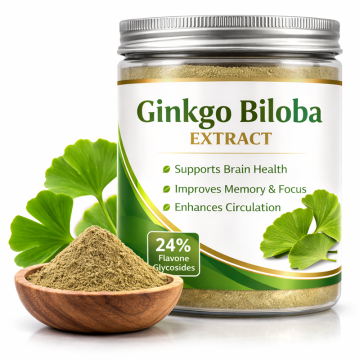 Ginkgo Biloba Extract 50:1 - Rich in Flavone
 Centella Asiatica Extract for Skin Rejuvenation
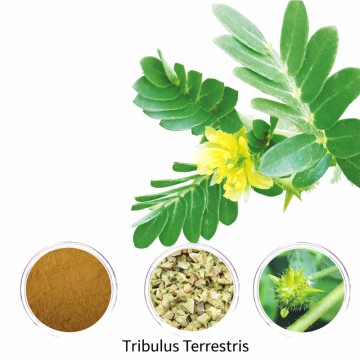 Tribulus Terrestris Extract 10:1 4:1 Saponins
 Astragalus Extract Standardized Immune Support
Tribulus Terrestris Extract High Quality Saponins
Standardized Astragalus Extract Powder China
 China Magnolia Extract Standardized Oral Health